- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- Italiano
- Nederlands
- 한국어
- Svenska
- Dansk
- Suomi
- Gaeilge
- Indonesia
- Norsk
- český
- український
- Қазақша
- Euskal
- Srpski језик
- tiếng Việt
- ภาษาไทย
- Polski
- magyar
- Malay
- বাংলা ভাষার
- हिन्दी
- Pilipino
- Türkçe
- العربية
- تمل
- ελληνικά
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी

GY Is Building Its Own In-House QC Lab - Engineered to CSA Standards
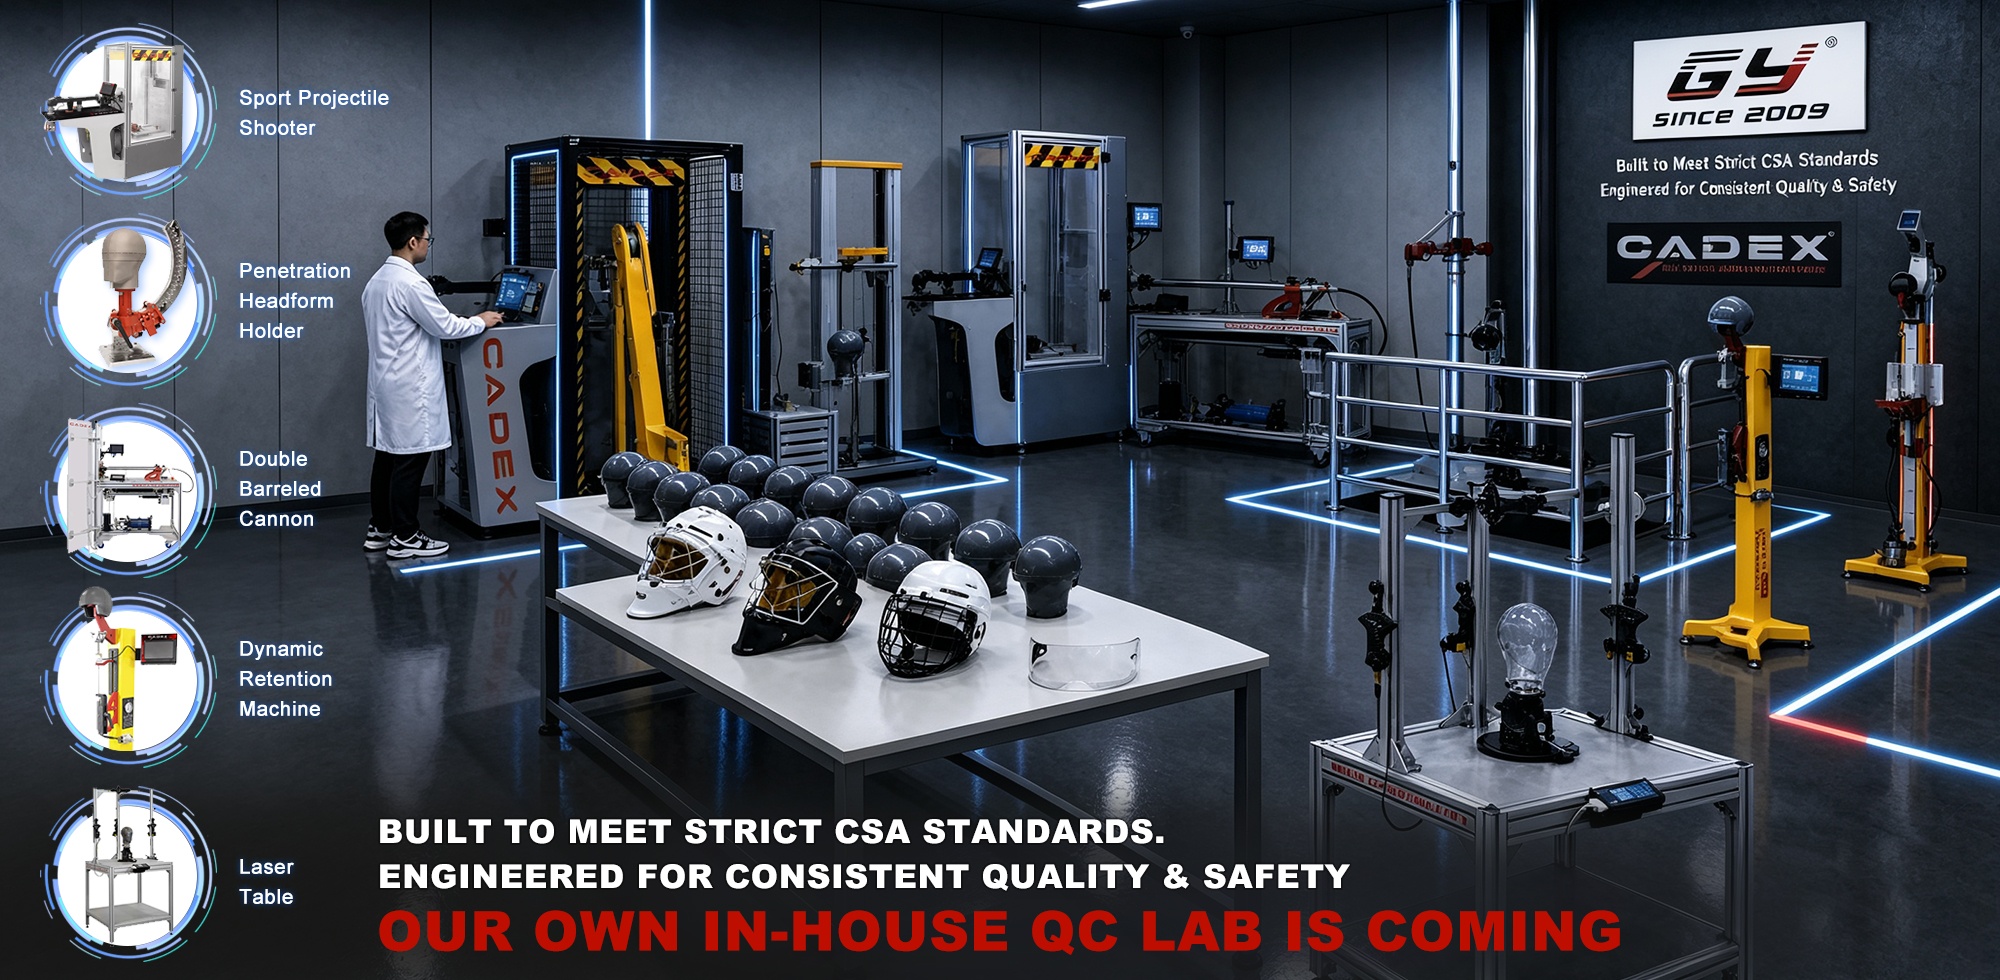
GY is fully committed to establishing an in-house quality control laboratory in strict compliance with CSA standards. Once running, we can test our own ice hockey helmets, cages and visors on every production batch — not just on samples before a certification submission.
For buyers, that changes the one thing that matters: how early a defect gets caught.
Why Now
Third-party test slots are scarce, expensive and slow — one round trip can cost one to three weeks. When a result comes back marginal, the tooling has already run and the shipping window is gone.
An in-house lab doesn't replace accredited certification. It removes the guesswork before it.
Stated plainly: our lab is a pre-verification facility. Formal CSA certification is issued only by accredited bodies and ISO/IEC 17025 laboratories. We built ours to replicate those methods so what we ship behaves like what we submit.
What CSA Requires
|
Standard |
Applies to |
Key requirements |
|
CSA Z262.1 |
Helmets |
Construction, penetration, shock absorption, retention, field of view, marking |
|
CSA Z262.2 |
Face protectors (cages, visors) |
Coverage, impact resistance, field of view, attachment, marking |
A helmet-plus-cage combination carries two obligations, not one — ask any supplier to show you both labels. On shock absorption, published CSA Z262.1 test protocols use a 275 g peak linear acceleration ceiling as the failure criterion.
Sources: CSA Group · ANSI Blog · IRCOBI
Five Stations, Five Failure Modes
|
Equipment |
What it proves |
Catches |
|
Sport projectile shooter |
Cracking at mounting holes, wire deflection into the eye zone |
|
|
Double-barreled cannon |
High + low velocity in one rig |
Materials that pass at one energy level and fail at another |
|
Penetration headform holder |
No sharp object reaches the head |
Shell thinning at vents, weak points at the mould gate |
|
Dynamic retention machine |
Chin strap holds under shock load |
Buckle slip, strap stretch, anchor tear-out |
|
Laser table |
Reference planes on the headform |
Measurement drift — the reason two technicians get two results |
What Changes for Buyers
|
|
Outsourced only |
With in-house lab |
|
New mould feedback |
1–3 weeks |
Same day |
|
Test frequency |
Before submission |
Every batch |
|
Material substitution risk |
Found after shipment |
Found before mass production |
|
Your compliance file |
Certificate only |
Certificate + batch records |
Because mould design, production and testing sit in the same building, a failed retention test on Tuesday becomes a revised buckle anchor on Wednesday.
GY since 2009 — 20+ R&D staff, 10,000 m² factory, exporting to 20+ countries. See our helmets or about GY.
FAQ
Can GY issue its own CSA certification?
No — and question any supplier who claims otherwise. Our lab is for internal verification and pre-submission screening, which raises first-pass success rates.
Difference between Z262.1 and Z262.2?
Z262.1 covers the helmet; Z262.2 covers the face protector. Sold together, you need both markings.
Can you provide test data for my order?
Yes — internal batch records alongside third-party certificates. Send an inquiry with your model and target market.
Does in-house testing raise unit price?
It lowers the costs that actually hurt: failed submissions, rework and delays.
When will the lab be operational?
In active build-out. Ask for the current timeline or schedule a factory visit.
Talk to Us Before Your Next Run
The time to align on test methods is before tooling, not after the first container.
Tell us: (1) target market and standard, (2) category and annual volume, (3) private label or stock model.
👉 Send an inquiry to GY Hockey https://www.gyhockey.com/— our engineering team answers technical questions directly.
Zhuhai GY Hockey Co., Ltd. — ice hockey head and face protection since 2009.